
Bonding Wire Sizes and Selection
Bonding Wire Selection: What considerations are needed to be taken into account when selecting a wire for wire bonding? (IKB-037)
Selecting the correct bonding wire is critical to achieving reliable, repeatable wire bonds in microelectronics assembly. Wire choice directly affects bond quality, electrical performance, long‑term reliability, and process stability.
Wire choice is influenced by electrical requirements, bond pad geometry, bonding process capability, and material compatibility.
Key Selection Criteria:
When specifying a bonding wire, the following parameters must be defined and understood.
- Wire diameter
- Bonding wire materials & purity
- Mechanical properties
- Wire spool size
Each parameter influences both bond quality and process stability.
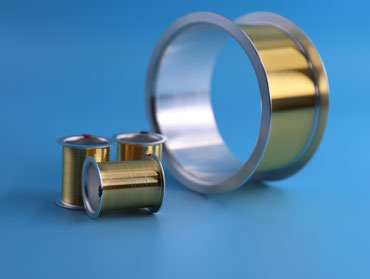
Wire Diameter:
Bonding wire diameters typically range from 12.5 microns to 500 microns.
- 12.5 to 75 microns
Considered fine wire bonding, commonly used in general semiconductor and high-density applications. - 100 to 500 microns
Considered large or heavy wire bonding, typically used for power devices, discrete components, battery connections and high current interconnects.
Wire diameter is usually determined by the circuit (such as current-carrying capability and frequency required) or component requirements and tolerances (such as bond pad size, pitch and length).
Wire pad size, position and pitch will greatly affect the constraints of the maximum wire diameter that can be used. The greater the outside wire diameter the larger the bonding tool will need to be, the larger the tool the more clearance is needed between bonds, directly affecting the minimum pitch size that can be bonded. Other factors that will need to be considered are the fusing current, electrical resistance, thermal conductivity and active impedance for high frequency applications.

Bonding Wire Materials & Purity:
Bonding wires are manufactured from metals with high electrical conductivity, using the highest purity materials that are precisely doped and annealed to achieve the required grain structure and mechanical properties.
Material selection is usually driven by process compatibility, electrical performance and cost. The most commonly used materials are:
- Gold
- Aluminium
- Copper
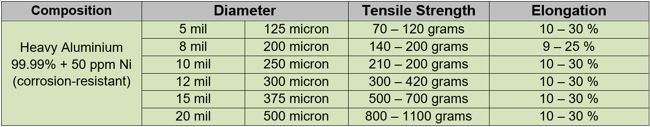
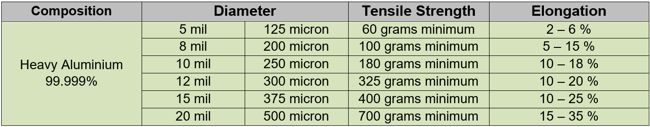
Large aluminium bonding wire for heavy wire applications (typically 100 – 500 microns) and ribbon generally has a purity of either 99.99% or 99.999%.
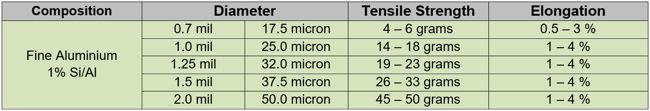
Fine aluminium bonding wire (typically 17 – 75 microns) is an alloyed wire, containing 1% silicon (1%SiAl) in order to help prevent silicon migration from a bonded semiconductor die, which could result in a deterioration in bond quality and durability, as well as loop shape stability.
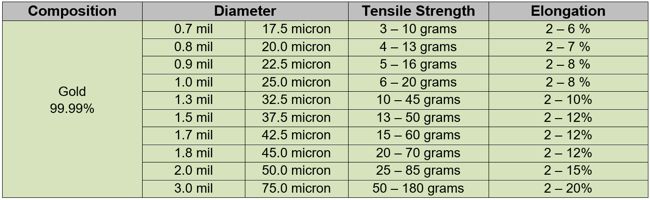
Gold bonding wire used in fine wire applications (typically 12.5 to 75 microns), is manufactured from 99.99 percent pure gold with controlled doping additives. These additives enable high speed automatic bonding and consistent bond and loop formation.
Other materials can be used and found in wire bonding for specific applications, examples of which are silver, platinum, palladium, and some coated wires. These materials are often selected for enhanced electrical performance, improved reliability, or reduced material cost.
Mechanical Properties:
The mechanical properties of bonding wire vary depending on the bonding process and application.
- Tensile strength affects wire handling, bond pull strength, and resistance to deformation.
- Elongation influences loop formation, stress absorption and resistance to fatigue during thermal cycling.
Different bonding processes, such as ball bonding, wedge bonding, and ribbon bonding, require different balances of tensile strength and elongation to achieve stable and repeatable bonds.
For example, the specification of a 25µm gold wire for a thermosonic ball bond is different from that needed to make a thermosonic wedge bond. As the looping profiles on a ball bond will be usually higher compared to a wedge bond, then having a wire that is stable at higher loops is more critical in your wire selection – the higher and more stable the wire is at looping could mean a compromise in strength and / or reliability. The 25µm gold wire that has been thermosonic wedge bonded will usually have lower loops that need to be stable and have lower impedance for high frequencies applications. The wire will be doped, annealed and tooled to suit these characteristics. Each desired criteria of the wire will affect the bonding performance in some way so research into the wire’s datasheet is essential.
Fusing Currents:
The fusing current is the minimum electrical current that heats a wire to its melting point, causing the conductor to fuse (break). It is a critical parameter for circuit protection and wire sizing, linking electrical loading to thermal failure limits.
Determining the fusing current helps engineers prevent overheating-related wire failures by accounting for material thermal and electrical properties.
Gold: Has superior corrosion resistance and high conductivity; cost and weight are limiting factors.
Aluminium: Lightweight and cost-effective. Lower conductivity than copper and gold, but suitable for large-scale power transmission.
Copper: Offers excellent electrical conductivity and mechanical strength but is more difficult to wire bond due to harder material properties and tendency to oxidise.
The following table of “Maximum Wire Bond Currents” is for indicative purposes only, based on wire lengths > 0.040”, and per Mil-H-38534.

Grain Structure:
Grain structure can affect the properties of the wire bond being made.
In power electronic circuits, grain boundary behaviour in aluminium wire bonds directly affects maximum continuous current capability, thermal cycling lifetime, resistance drift over life, and failure mode predictability. In ball bonding applications, during the ball formation, the grain structure of the wire directly above the FAB (free air ball) is altered. The heat affected zone (HAZ) is mechanically weaker than the original wire, so this directly affects the loop formation and stability. A fine grain structure introduces a shorter HAZ providing lower loop heights. A long HAZ assists in loop shapes that are naturally higher without relying on the capillary trajectory.

Wire Spool Size:
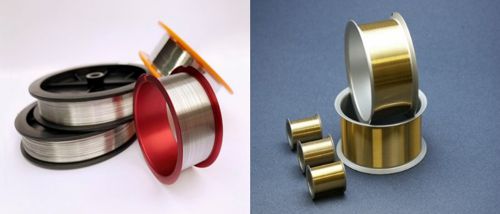
Correct spool choice helps maintain consistent wire feed and reduces the risk of handling damage or contamination.
There are two main considerations to consider when specifying what spool type you need for your bonding wire. The first is the spool type itself, which needs to be compatible with the wire bonding system you are working with. As the wires are subject to contamination which can affect bond quality and strength, as well as the fine nature of the wire, reworking or re-spooling the wire is not recommended, making the spool specification more critical.
The second criterion to consider is the length of the wire required on the spool as well as how many layers being wound. Multi-wound spools that have more than one layer of wire wound onto the spool will hold an increased length of wire, but this increases the risk of wire becoming snagged from the spool as it is fed into the wire bonding machine. Fine wire SiAl is more prone to becoming snagged if oxide layers start to form from incorrect storage. This is especially true for small bobbin-like spools that have multiple wires, as this wire tends to have “memory” so it will try to return to the wound shape if left unused on the machine for too long.
For manual wire bonding machines, it is recommended to use a single wound layer to prevent this. If using a fully automatic wire bonder, then changing wire spools means additional down time which will affect production and throughput each time a machine is stopped for a spool change, so a multi-wound spool may be more desirable.

Practical Selection Checklist
Before specifying a bonding wire, confirm the following:
- Bond pad material, size, and pitch are compatible with the selected wire diameter
- Electrical current and frequency requirements are met
- Bonding equipment and tooling support the chosen wire material and size
- Mechanical properties align with the intended bonding process
- Environmental and reliability requirements are satisfied
Summary
Bonding wire selection is a balance between electrical performance, mechanical behaviour, process capability, and cost. Correct specification ensures reliable interconnects, stable bonding processes, and long-term device performance.
View the range of “Coining Wire Bonding Materials“.
Author
Date
Version
Author
Adam Marshall
Date
28 April 2020
Version
IKB037 Rev. 3
Download
Author Biography
Adam Marshall is a Senior Technical Support Engineer at Inseto Ltd with over 14 years of experience in the semiconductor industry, including 10 years specialising in assembly processes and related equipment. He supports customers across the microelectronics and semiconductor sectors who rely on precision equipment to maintain reliable and repeatable results in production and research environments.
Known for a calm and structured approach, Adam works closely with customers, suppliers and internal teams to deliver clear technical advice and dependable support when it matters.
 Back to top